
Valley Restoration Pros delivers 24/7 industrial emergency water extraction, thermal psychrometric drying, and structural mitigation across Phoenix and Maricopa County with guaranteed 30–60 minute rapid arrival. All protocols strictly adhere to IICRC S500 standards, featuring upfront itemized pricing and free on-site thermal moisture assessments. Call dispatch directly at (602) 847-9593.
Why Immediate Mitigation Is Critical in Phoenix Heat
Subterranean airport baggage handling tunnels and automated sortation vaults face severe inundation during Phoenix monsoon deluges and tarmac sheet-flow runoff. Floodwaters submerge 480V 3-phase motor control centers, high-speed diverters, optical barcode scanning arrays, and TSA inline explosives detection systems (EDS). In 115°F desert heat, trapped subterranean moisture creates a corrosive 95%+ relative humidity microclimate, triggering rapid electrical arc faults, conveyor bearing seizure, and Category 3 contamination with aviation fuels, tarmac silt, and caliche sediments, threatening catastrophic flight cancellations and FAA ground delays.
Service Definition & The IICRC Standard of Care
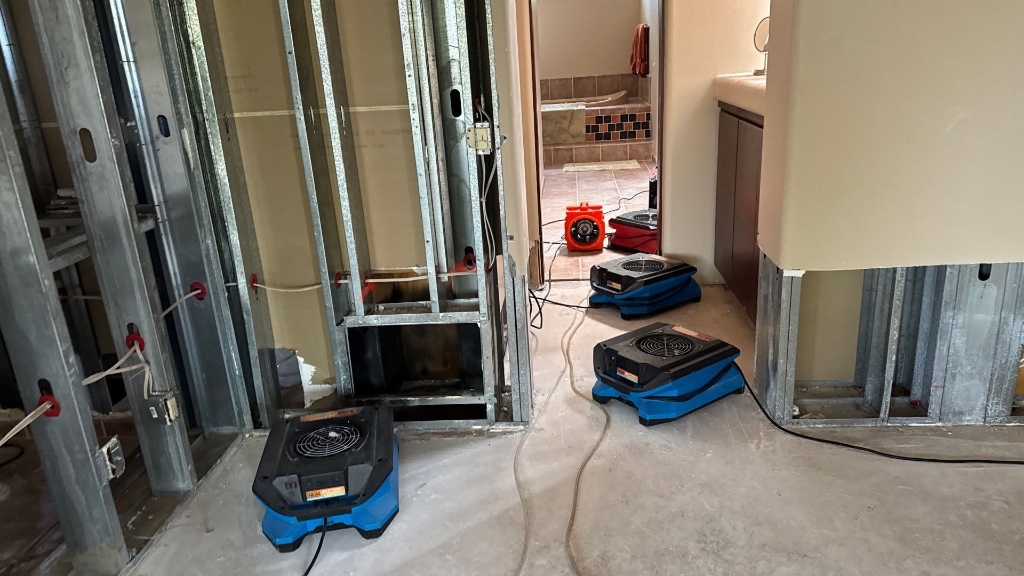
Professional commercial airport baggage handling tunnel flood phoenix is an engineering and environmental discipline adhering strictly to IICRC S500 protocols, not mere surface mopping. When structural plumbing failures strike in Maricopa County, certified emergency water extraction and thermal structural drying procedures must be deployed immediately. Whether triggered by high-pressure burst pipe emergencies, subfloor leaks, or commercial line ruptures, bound moisture rapidly penetrates concrete subfloors and wall framing. In the desert heat, delays trigger microbial proliferation requiring rapid mold remediation. Request damage assessment through our emergency assessment portal or request 30-minute dispatch across all Valley service areas.
Securing electrical feeds, inspecting load-bearing assemblies, and containing pathogens.
Stopping the intrusion source and erecting 6-mil plastic isolation containment airlocks.
31-HP truck-mount extraction, removing gallons exponentially faster than evaporation.
LGR dehumidifiers and HEPA air scrubbers driving grains per pound below 25 GPP.
Calibrated electronic pinless testing confirming baseline dry standards.
The Complete 6-Stage Restoration Roadmap
Our IICRC-certified crews execute a disciplined, scientific 6-stage protocol to stabilize and dry structural components:
Emergency Dispatch & Perimeter Isolation
30 to 60 minute arrival. Securing electrical shutoffs, evaluating structural loads, and erecting containment airlocks.
FLIR® Thermal Mapping & Baseline Scans
Infrared thermal scans detect trapped moisture behind walls and beneath concrete without invasive exploratory demolition.
High-Volume Bulk Extraction
31-HP truck-mount extraction units pump standing water away at hundreds of gallons per minute.
Controlled Selective Demolition
Precision flood cuts 12 to 24 inches above moisture lines, removing wet insulation and opening wall framing to dry airflow.
Thermodynamic Dehumidification
Industrial Low-Grain Refrigerant dehumidifiers pull deep trapped moisture from dense framing lumber and concrete slabs.
Antimicrobial Sanitization & Verification
EPA-registered botanical application (Benefect Decon 30) and calibrated moisture testing to issue an official dry certificate.

Specialized Equipment & Industrial Restoration Technology
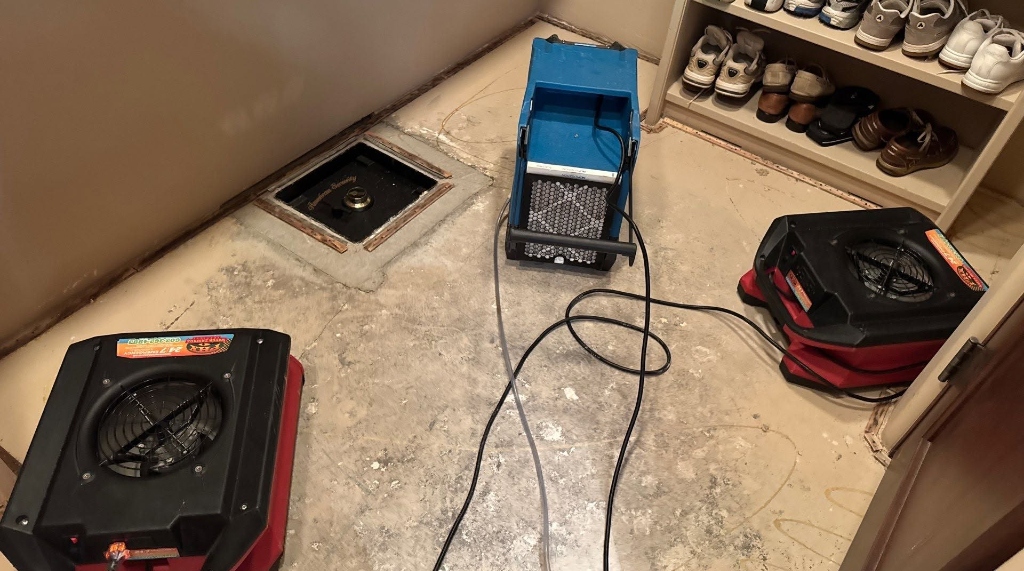
Mitigating severe property damage requires industrial-grade technology capable of altering thermodynamic psychrometrics:
Truck-Mounted Extraction Rigs
31-HP engines producing 16+ inches Hg vacuum suction to evacuate bulk water rapidly into holding tanks.
Low-Grain Refrigerant Dryers
Pre-cooling heat-pipe systems driving ambient grains per pound below 25 GPP to draw deep trapped water out of framing.
HEPA Negative-Air Scrubbers
Hospital-grade 99.97% particulate filtration capturing microscopic fungal spores, soot, and biohazard aerosols.
FLIR® Thermal Scanners & Probes
Infrared thermography detecting evaporative cooling boundaries behind walls, combined with digital RF pinless scanners.
Professional Restoration vs. DIY Mitigation
Attempting DIY cleanup during a property disaster creates severe hidden liabilities:
- Trapped Moisture: Surface drywall dries while moisture inside cavities triggers hidden mold blooms.
- Pathogenic Risks: Category 2 & 3 water contains bio-contaminants standard cleaners fail to kill.
- Insurance Denial: Insurers require daily psychrometric logs; lack of data causes claim disputes.
Transparent Upfront Itemized Pricing
Valley Restoration Pros operates with complete transparency:
- Free On-Site Assessment: Complete physical inspection before work begins.
- Upfront Itemized Estimates: Detailed line items calculated via industry-standard Xactimate.
- Zero Surprise Billing: No hidden charges or unauthorized repairs.
Certified commercial airport baggage handling tunnel flood phoenix Field Documentation
Every response performed by Valley Restoration Pros is documented through photographic and thermographic records:

Comprehensive commercial airport baggage handling tunnel flood phoenix Technical Manual & Operational Standards
Exhaustive engineering protocols, psychrometric calculations, geological multipliers, and step-by-step restoration standards for Maricopa County properties:
Executive Emergency Abstract: Subterranean Airport Baggage Tunnel Inundation & Automated Sortation Dewatering
Within major commercial aviation facilities and regional air transportation hubs across Greater Phoenix—anchored by Phoenix Sky Harbor International Airport (PHX), Phoenix-Mesa Gateway Airport (AZA), and the high-capacity corporate flight centers of Scottsdale Airport (SDL) and Deer Valley Airport (DVT)—subterranean baggage handling tunnels represent mission-critical logistical arteries. Positioned deep beneath terminal ramp aprons, commercial gate concourses, and active taxiways, these reinforced concrete subterranean networks house multi-million-dollar automated Baggage Handling Systems (BHS). Spanning miles of continuous high-speed belt conveyors, automated tray sorters, vertical continuous lifts (VCLs), high-speed diverter pushers, and Transportation Security Administration (TSA) checked baggage inspection system (CBIS) matrices, this infrastructure operates under continuous, high-throughput operating demands.
When extreme Sonoran Desert meteorological events occur—specifically violent summer monsoon microbursts, convective cell thunderstorms, and torrential sheet-flow runoff across thousands of acres of non-porous asphalt and concrete tarmac—these below-grade tunnels face severe, rapid inundation. Because subterranean baggage tunnels and tug transit corridors sit below the surrounding grade and local hydraulic water table, surface water cascades through exterior tug drive portals, open conveyor transfer chutes, and compromised perimeter expansion joints at velocities exceeding thousands of gallons per minute. Within minutes, below-grade utility trenches, conveyor drive pits, and cast-in-place concrete maintenance tunnels become completely submerged.
The operational and financial ramifications of an unmitigated subterranean airport baggage tunnel flood are immense. When standing water reaches automated conveyor drive assemblies, electric induction motors, variable frequency drive (VFD) enclosures, and optical automatic tag reader (ATR) barcode scanner arrays, sorting operations instantly grind to a dead halt. Airlines face immediate baggage handling gridlock, thousands of stranded passenger bags, tarmac congestion, and crippling FAA flight delays. Airline delay costs routinely exceed $150,000 per hour in passenger accommodation penalties, FAA ground delay program fines, and emergency carrier rerouting expenses.
Furthermore, airport runoff is legally and biologically categorized as an aggressive Category 3 blackwater contamination event. Sheet flow sweeping across active airside aprons collects unburned Jet-A aviation fuel, hydraulic fluid, synthetic turbine lubricants, runway rubber residue, deicing fluid remnants, bird droppings, and dense alkaline caliche silt. When this hazardous chemical and biological slurry inundates confined subterranean tunnels during peak 115-degree Phoenix summer heat, the subterranean envelope transforms into a hazardous confined space with high atmospheric humidity, toxic aerosol dispersion, and rapid microbial incubation. Immediate deployment of certified commercial water damage specialists with industrial-scale extraction power is paramount to prevent permanent electrical destruction and restore air transportation velocity.
Immediate Airport Operations & Baggage Tunnel Incident Directives
- Initiate Confined Space Lockout & High-Voltage Electrical Isolation: Immediately trip master circuit breakers supplying 480V 3-phase power to baggage conveyor drives, motor control centers (MCC), inline sorting diverters, and subterranean lighting sub-panels. Verify zero voltage potential before any personnel or equipment enter standing tunnel water.
- Establish OSHA Permit-Required Confined Space Protocol: Treat all flooded subterranean airport tunnels as permit-required confined spaces under OSHA 1910.146. Station dedicated safety sentries at every access portal, enforce 4-gas continuous atmospheric monitoring (oxygen, LEL combustible hydrocarbons, carbon monoxide, and hydrogen sulfide), and maintain calibrated ventilation blowers.
- Protect TSA Checked Baggage Inspection (CBIS) Arrays: Immediately isolate inline computed tomography (CT) explosive detection systems (EDS), automated tag reader (ATR) camera housings, and pneumatic diverter valves from incoming moisture pathways with impermeable magnetic fluid shields and temporary flood diversion dikes.
- Mobilize Specialized Industrial Aviation Restoration Units: Contact commercial aviation operations director Marcus Vance at the Valley Restoration Pros 24/7 Commercial Aviation Rapid Dispatch Center at (602) 847-9593. Our certified industrial response crews arrive within thirty minutes equipped with diesel high-flow trash pumps, explosion-proof negative air extraction, and trailer-mounted desiccant dehumidification systems.
For critical airfield dewatering operations requiring high-volume pumping, our team coordinates seamlessly with airport operations personnel to deploy emergency water extraction assets across flooded subterranean infrastructure without interrupting airfield operations.
Anatomy of Subterranean Tunnel Inundation: Hydraulic Flow, Sump Failure & Mechanical Corrosion
Modern airport baggage handling systems represent intricate networks of electro-mechanical, pneumatic, and computer-controlled sorting hardware operating in confined concrete tunnels beneath airport terminals. Understanding the destructive hydraulic flow patterns and mechanical vulnerabilities that arise during a subterranean flood event is critical to engineering an effective, rapid-turnaround recovery plan.
Portal Inflow & Sump Inundation
Subterranean tunnels feature inclined tug ramps, baggage drop chutes, and ventilation shafts that connect directly to surface tarmac ramps. When rainfall rates exceed tarmac storm drain retention capacities, stormwater cascades downward along the path of least resistance. Subterranean lift stations, typically equipped with duplex 5-horsepower submersible sump pumps, are designed to handle routine pipe condensation and minor washdowns—not torrential inflows of 3,000 to 5,000 GPM. Sump pits overflow within minutes, floating electrical control floats, shorting mechanical relays, and converting low points into stagnant flood reservoirs.
Electric Motor & VFD Ingress
Baggage handling lines utilize high-efficiency 480V 3-phase induction drive motors coupled to heavy-duty planetary gear reducers positioned at floor level or within subterranean drive pits. As floodwater rises above equipment mounting beds, silt-laden water penetrates motor stator windings, bearing seals, and terminal junction boxes. Submerged gear reducers suck in contaminated water through pressure relief breathers as hot gearboxes cool rapidly in floodwaters. Variable Frequency Drive (VFD) enclosures located along tunnel walls suffer catastrophic PCB board corrosion and electrolytic short-circuit destruction.
Conveyor Belt Delamination & Roller Seizure
Automated sortation lines utilize multi-ply polyester and polyurethane conveyor belting running across thousands of precision steel idler rollers and motorized pulleys. Submersion in muddy water forces abrasive quartz and caliche particulates into sealed roller bearings. As water evaporates, fine abrasive silt hardens inside race grooves, causing total bearing lockup. Furthermore, moisture wicking into vulcanized belt splices initiates rapid ply delamination, causing belts to track off-center, stretch unevenly, and tear along drive drums under full motor torque.
Scanning Optics & PLC Controller Failure
High-speed sortation relies on Automatic Tag Reader (ATR) optical laser arrays and multi-angle camera gantries that scan IATA barcode tags on baggage traveling up to 600 feet per minute. Moisture condensation coats optical lenses with mineral films, blinding scan engines. Proximity sensors, photo-eyes, and Programmable Logic Controller (PLC) input/output racks installed in tunnel alcoves absorb airborne moisture, generating phantom fault triggers and shutting down automated pneumatic diverter pushers throughout the entire facility matrix.
Vertical Continuous Lift (VCL) Vault Hydraulic Failure
Vertical Continuous Lifts (VCLs) transport checked luggage vertically between subterranean conveyor tunnels and main terminal ticketing hall check-in counters. These vertical shafts sit in deep recessed pits that act as subterranean natural sumps. Silt and floodwater inundate lift vertical track rails, counterweight sheaves, carriage lift chains, and hydraulic buffering pistons. Caliche silt grinds away mechanical chain pins, causing catastrophic jamming of vertical luggage carriages and blocking outbound bag induction.
Underground Cable Tray & Busway Silt Contamination
Subterranean tunnel corridors carry thousands of linear feet of open ladder cable trays and enclosed busways transmitting 480V distribution power, 120V control wiring, and high-speed fiber communication loops. Standing water and sediment slurry settle into bottom cable trays, encasing power feeds in caustic, conductive mud. Even after standing water recedes, trapped mud retains moisture against jacketed insulation, accelerating dielectric breakdown and causing ground fault alarms across the entire facility.
When flood events originate from sudden meteorological deluges on the tarmac, facility directors should explore our specialized technical procedures for storm flood cleanup to address exterior perimeter runoff pathways concurrently with subterranean dewatering.
Similar deep subterranean hydraulic dynamics occur in commercial vehicle parking structures beneath passenger terminals. Property managers can review our dedicated protocols for subterranean parking garage flood extraction for additional insight into managing heavy sub-grade water intrusion.
Phoenix Climatic & Geological Multipliers: Caliche Silt, Runway Runoff & 115°F Subterranean Humidity
Executing a structural dewatering and equipment desiccation operation within an airport baggage tunnel in Greater Phoenix involves environmental and physical conditions unique to the Sonoran Desert. The convergence of extreme surface heat, expansive clay subsoils, and chemical-heavy apron runoff requires tailored engineering methodologies:
1. Micro-Burst Monsoon Deluges & Impervious Airfield Sheet Flow
From late June through September, the North American Monsoon generates intense localized convective storms across Maricopa County. Airfield environments present thousands of continuous acres of impervious asphalt and concrete runways, taxiways, and terminal ramps. During a microburst dropping 2.0 to 2.5 inches of rain within forty-five minutes, runoff volumes completely overwhelm perimeter catch basins and oil-water separators.
This high-velocity surface water pools rapidly against terminal foundations, overflowing ramp thresholds and entering baggage tunnel intake corridors. Unlike municipal rainfall that flows into natural soil channels, 100% of airfield rain becomes energetic surface runoff loaded with heavy debris.
2. Expansive Caliche Soil Hydrostatic Uplift & Structural Joint Seepage
The Salt River Valley basin is underlain by dense alluvial soil beds containing thick layers of caliche—a sedimentary rock-like cementation of calcium carbonate, clays, and silt. In dry conditions, caliche is hard and impermeable. However, when sudden deluge waters saturate the sub-base, surrounding expansive smectite clays expand with massive hydrostatic uplift pressures exceeding 8,000 pounds per square foot.
This intense lateral and vertical pressure forces groundwater through below-grade construction cold joints, expansion seams, seismic isolators, and utility conduit penetrations. Fine caliche clay particulates are carried into the tunnels, depositing a dense, cementitious abrasive mud layer over conveyor beds and floor drains that cannot be cleared with simple wet vacuums.
3. 115°F Desert Ambient Heat & Subterranean Vapor Condensation Traps
Phoenix summer temperatures routinely surpass 115 degrees Fahrenheit on the airfield ramp, heating surface asphalt to over 160 degrees. Below ground, concrete tunnel walls maintain a cooler thermal mass between 75 and 82 degrees Fahrenheit. When standing floodwaters enter these warm subterranean tunnels, rapid evaporation produces internal relative humidity levels exceeding 95% with humidity ratios over 160 grains per pound (GPP).
Because these tunnels lack exterior windows and standard HVAC airflow, moisture becomes trapped in a superheated vapor bubble. The dew point rises above the temperature of exposed steel conveyor frames, electrical conduits, and chilled water pipes, causing continuous condensation to rain down from the ceiling onto sensitive electronics, causing rapid rust blooming on unpainted mechanical surfaces within twelve hours.
4. Jet Fuel Hydrocarbons & Extreme 18–24 GPG Municipal Water Chemistry
Airfield runoff does not consist of clean rainwater; it carries accumulated Jet-A kerosene hydrocarbons, aviation hydraulic fluids (polyalphaolefin and phosphate ester fluids), rubber residues from aircraft tires, and high concentrations of dissolved minerals. Greater Phoenix municipal water supply lines and runoff carry extreme mineral hardness between 18 and 24 grains per gallon (GPG) dominated by calcium and magnesium bicarbonates.
When this caustic, hydrocarbon-laced chemical cocktail contacts electrical switchgear and steel conveyor linkages, it forms an aggressive electrolyte solution that accelerates galvanic corrosion across dissimilar metals. In scenarios where pressurized chilled water lines or domestic fire mains rupture inside airport tunnels, refer to our specialized breakdown for burst pipe repair and containment. If sanitary lines back up during flooding, view our protocols for sewage cleanup and biohazard sanitization.
Immediate First-Hour Emergency Protocol: Confined Space Isolation & Airfield Operations Security
The initial sixty minutes following water intrusion into a subterranean airport baggage tunnel dictate whether an airport terminal resumes normal flight sortation within twenty-four hours or suffers catastrophic multi-day flight cancellations and multimillion-dollar equipment replacement. Airport operations managers, terminal engineering personnel, and airline ground handling directors must execute an immediate, disciplined sequence of containment procedures:
Phase 1: Confined Space Life Safety & Atmospheric Hazard Verification (Minutes 0–15)
Immediately sound evacuation horns for all baggage handlers, tug operators, and maintenance technicians inside the subterranean tunnel complex. Restrict all entry points under OSHA Permit-Required Confined Space standards (29 CFR 1910.146). Station designated safety attendants at every tunnel portal. Deploy calibrated 4-gas atmospheric monitors to measure lower explosive limits (LEL) for volatile aviation hydrocarbons, oxygen concentrations (must remain between 19.5% and 23.5%), hydrogen sulfide, and carbon monoxide before any dewatering personnel enter the zone.
Log initial atmospheric readings in the official Airside Confined Space Entry Registry. Verify that continuous forced-air mechanical ventilation is running at a minimum of 20 air changes per hour (ACH). If hydrocarbon vapors exceed 10% of the Lower Explosive Limit (LEL), prohibit entry and deploy intrinsically safe explosion-proof ventilation equipment immediately.
Phase 2: High-Voltage Electrical Lockout/Tagout & Motor De-Energization (Minutes 15–30)
Facility master electricians must immediately execute Lockout/Tagout (LOTO) protocols at the main distribution sub-station supplying the baggage tunnel. De-energize 480V 3-phase feeder lines supplying Motor Control Centers (MCC), conveyor drive drums, hydraulic diverter power units, and floor sump lift stations. Water contact with 480V busbars causes explosive arc flash incidents capable of destroying electrical switchgear and endangering personnel. Lock out and tag all sub-panel breakers until certified master restorers verify complete dryness.
De-energize uninterruptible power supply (UPS) batteries serving Programmable Logic Controller (PLC) racks and Automatic Tag Reader (ATR) barcode cameras to prevent reverse electrical feed into submerged circuits. Apply padlock lockout tags on all main breaker handles and maintain possession of keys under the control of the incident safety officer.
Phase 3: Surface Water Diversion & Ramp Ingress Containment (Minutes 30–45)
Airport ground maintenance crews must immediately deploy heavy-duty rubber spill berms, polyurethane flood barriers, and weighted sandbag dikes at surface tug ramp portals, baggage intake doors, and tarmac ventilation grates to halt cascading surface runoff. If stormwater continues to pool on the exterior tarmac apron, deploy portable trench pumps to redirect water toward secondary retention basins. For advanced structural preservation techniques, see our detailed specifications for structural drying.
Position emergency vacuum tankers on the airside service road to intercept sheet flow before it reaches below-grade portal thresholds. Seal exterior conveyor return slots with magnetic industrial neoprene storm blankets to prevent external water backflow into internal sortation halls.
Phase 4: SIDA Security Coordination & Industrial Restorer Dispatch (Minutes 45–60)
Notify TSA Airport Security Directors and airport police to establish expedited vehicle access through airside security access gates (AOA perimeter gates). Coordinate SIDA badge escort protocols for incoming industrial restoration equipment. Call Valley Restoration Pros at (602) 847-9593 to mobilize dedicated commercial aviation disaster units equipped with SIDA-badged supervisors, self-powered diesel trash pumps, and large-tonnage desiccant dehumidifiers.
Establish an Incident Command Post at the terminal ground support operations center. Designate dedicated staging zones on the airside service apron for industrial desiccant trailers, fuel delivery trucks, and high-volume wastewater disposal tankers to maintain clear vehicle taxiway corridors.
Industrial Equipment Deployment: High-Volume Dewatering & Low-Grain Desiccant Systems
Subterranean airport baggage tunnels present unique logistical hurdles: narrow physical clearances, restricted ventilation, Class 1 Division 1 hazardous atmosphere potential from aircraft fuels, and high electrical density. Standard commercial restoration tools are entirely inadequate. Valley Restoration Pros deploys purpose-built, heavy industrial machinery designed specifically for below-grade critical infrastructure recovery:
Trailer-Mounted Industrial Desiccant Systems
Model: Aggreko / Munters 5,000 to 10,000 CFM Industrial Desiccants
These self-contained diesel-powered trailer units utilize solid silica gel rotor wheels to extract moisture regardless of ambient temperature. By ducting ultra-dry process air (delivering under 15 grains per pound and relative humidity below 10%) hundreds of feet into subterranean baggage tunnels while venting hot, wet reactivation exhaust out to the surface apron, these systems rapidly pull moisture from concrete vaults and conveyor drives without elevating subterranean heat.
Hydraulic Submersible & Diesel Trash Pumps
Capacity: 6-Inch Godwin CD150M Dri-Prime / Wacker Neuson Submersibles
Discharging up to 1,800 gallons per minute against 150 feet of vertical head, these solids-handling trash pumps easily pass 3-inch spherical solids, caliche mud, and shredded luggage debris. Outfitted with heavy-duty lay-flat discharge hoses, they lift floodwater out of deep conveyor pits directly into airport environmental retention interceptors without generating hazardous exhaust inside the tunnel envelope.
Explosion-Proof Axial Air Movers & HEPA Filtration
Model: Allegro Class 1, Division 1 Blowers & Dri-Eaz DefendAir HEPA Units
Because aviation fuel vapors can accumulate in confined below-grade spaces, non-sparking, intrinsically safe explosion-proof blowers are mandatory for air exchange. These units deliver up to 2,500 CFM of high-static pressure airflow through anti-static conductive ducting, exhausting combustible fumes while HEPA filtration scrubbers capture aerosolized hydrocarbon particulates and microbial contaminants.
Electronic Diagnostic & Insulation Resistance Testers
Hardware: Fluke 1587 FC Megohmmeter & FLIR E96 Thermal Cameras
Before any electric conveyor motor or MCC panel is re-energized, certified electrical technicians apply digital insulation resistance testing at 1,000 volts DC to verify that stator windings exceed 50 megohms to ground. High-resolution FLIR thermal cameras map subsurface moisture migration within concrete tunnel cold joints and detect residual moisture pockets inside electrical junction boxes.
Confined Space Tri-Pod Winch & Rescue Systems
Apparatus: DBI-SALA Salalift II Confined Space Rescue Systems & Type 3 SRLs
Permit-required subterranean baggage shafts demand dedicated mechanical retrieval apparatus. Our teams deploy certified aluminum tripod systems equipped with 60-foot galvanized steel retrieval cables, automatic fall-arrest self-retracting lifelines, and emergency winches positioned over all vertical utility maintenance hatches and conveyor service shafts.
High-Pressure Thermal Hydro-Extraction Rigs
Specs: Trailer-Mounted Hydro-Force 3,000 PSI at 210°F Closed-Loop Recovery
Eliminating caked caliche clay and oily apron sediments from conveyor drive tracks requires superheated water. Our trailer-mounted hydro-extraction systems deliver demineralized water heated to 210 degrees Fahrenheit at adjustable pressures up to 3,000 PSI, featuring closed-loop recovery heads that capture 99% of liquid effluent on contact to protect conveyor bearings and electrical conduit.
For deep mechanical sump pits and vertical continuous lifts (VCLs), explore our dedicated procedures for elevator pit water extraction to protect hydraulic rams and sub-grade mechanical systems.
For adjacent aviation properties such as maintenance facilities and corporate hangars, review our specialized services for aircraft hangar fire sprinkler discharge water extraction.
IICRC S500 9-Stage Baggage Tunnel Dewatering & Electro-Mechanical Recovery Protocol
Valley Restoration Pros executes an exhaustive 9-stage engineering restoration protocol adhering strictly to the IICRC S500 Standard for Professional Water Damage Restoration, FAA Advisory Circulars, and OSHA Confined Space regulations:
Stage 1: SIDA Airside Clearance, Confined Space Entry Permitting & Containment
Restoration leads verify all responding technicians hold active SIDA (Security Identification Display Area) badging or establish certified law enforcement escorts through airside security checkpoints. Technicians complete formal OSHA permit-required confined space entry documentation, establish mechanical ventilation providing 20 air changes per hour (ACH), verify LEL hydrocarbon safety levels, and install heavy 6-mil polyethylene dust and vapor containment barriers to isolate wet tunnel zones from passenger terminal concourses above.
Stage 2: High-Volume Hydraulic Submersible Dewatering
Crews lower heavy submersible hydraulic trash pumps into deep conveyor drive trenches, vertical lift pits, and main tunnel walkway troughs. Sump pumps extract thousands of gallons of standing water at rates up to 1,800 GPM. Wastewater is pumped through reinforced cam-lock discharge hoses to pre-designated airport industrial oil-water separators, ensuring total compliance with City of Phoenix industrial pretreatment and environmental discharge mandates.
Stage 3: Caliche Silt, Sludge & Aviation Hydrocarbon Slurry Extraction
Once standing bulk water is evacuated, a thick 2- to 6-inch sediment bed of caliche clay, tarmac sand, and fuel-contaminated sludge remains across conveyor frames and floor channels. Crews deploy industrial truck-mounted positive displacement vacuum extractors pulling 16 inches of mercury vacuum. Technicians thoroughly remove heavy sludge from underneath slider beds, return rollers, diverter paddles, and subterranean sumps.
Stage 4: Closed-Loop High-Pressure Decontamination & Rinse Cycle
Using softened, demineralized water heated to 200 degrees Fahrenheit, technicians execute controlled high-pressure closed-loop surface extraction. Specialized surface spinners simultaneously blast away caked caliche silt and synthetic grease deposits while instant vacuum recovery extracts 99% of wastewater on contact. This prevents overspray from impacting sensitive electrical conduit, optical photo-eyes, or TSA scanning portals.
Stage 5: EPA-Registered Antimicrobial & Hydrocarbon Emulsification Treatment
Because tarmac floodwater constitutes Category 3 blackwater carrying avian pathogens and fuel hydrocarbons, technicians apply an EPA-registered hospital-grade botanical disinfectant and hydrocarbon-neutralizing surfactant. Applied via electrostatic ULV foggers and low-pressure sprayers across non-electrical structural concrete, steel support stanchions, and drain trenches, this treatment eliminates microbial pathogens and neutralizes volatile organic compounds (VOCs).
Stage 6: Electric Motor, Gearbox & VFD Component Desiccation
Submerged 480V conveyor motors undergo specialized in-place restoration. Technicians unbolt motor end bells, flush stator windings with dielectric moisture-displacing solvents, and inspect bearing cavities. Contaminated synthetic gearbox oil is sampled, drained, and flushed with fresh lubricant. Targeted micro-drying enclosures are established over VFD cabinets, where heated, desiccated air is injected to safely pull moisture from circuit boards and terminal blocks.
Stage 7: Industrial Desiccant Psychrometric Drying Operation
Technicians deploy twin 7,500 CFM industrial desiccant dehumidifiers stationed on the service apron. High-volume lay-flat ducting channels ultra-dry process air (10% RH, 15 GPP) down through tunnel access portals. High-velocity axial air movers positioned every twenty feet establish a continuous vortex of drying air across conveyor framework and concrete walls, creating an intense vapor pressure gradient that extracts bound moisture into the airflow.
Stage 8: Structural Concrete Deep Desiccation & Micro-Capillary Moisture Extraction
Cast-in-place subterranean concrete tunnel walls absorb thousands of pounds of water through capillary action. Left unmitigated, this trapped moisture evaporates upward into passenger terminal subfloors, causing adhesive delamination and luxury vinyl tile (LVT) failure. Continuous low-grain desiccant drying continues for thirty-six to forty-eight hours until ASTM F2170 in-situ relative humidity probes confirm internal concrete moisture has dropped below baseline thresholds.
Stage 9: Megohmmeter Clearance Testing & TSA/FAA Operational Sign-Off
Before conveyor power is restored, certified electrical testing technicians execute insulation resistance tests across all motor phases and MCC bus connections using calibrated Fluke megohmmeters. All circuits must verify insulation resistance exceeding 50 megohms. In conjunction with TSA Checked Baggage Inspection System (CBIS) technicians, baggage lines undergo test bag runs, laser barcode verification, and emergency stop validation before formal FAA and airport operations clearance is signed.
TSA Security Matrix, Inline EDS Screening Systems & Electrical Decontamination
Subterranean airport baggage tunnels do not simply transport luggage; they integrate the Transportation Security Administration (TSA) Checked Baggage Inspection System (CBIS) and Checked Baggage Resolution Area (CBRA). The heart of this matrix includes multi-million-dollar computed tomography (CT) Explosives Detection Systems (EDS)—such as Smiths Detection CTX, L3Harris eXaminer, and Analogic ConneCT machines. These precision instruments feature high-speed rotating slip rings, sensitive multi-energy X-ray detector arrays, complex power distribution units (PDUs), and fiber-optic communication matrices that are acutely vulnerable to moisture and silt contamination:
EDS Machine Isolation & Micro-Enclosure Protection
When floodwaters enter the CBIS matrix, our team immediately erects sealed micro-containment enclosures around inline EDS machines. Because these multimillion-dollar systems cannot be exposed to raw liquid or aggressive humidity, dedicated HEPA filtered dehumidification air streams are channeled directly across machine gantries to prevent condensation from settling on high-voltage X-ray tube generators and sensitive scintillation detector diodes.
Optical Barcode Tag Reader (ATR) Array Reconditioning
High-speed sortation utilizes multi-head laser and CCD camera arrays to read IATA baggage barcode tags. In flooded tunnels, mineral-heavy caliche moisture evaporates onto optical lenses and glass mirrors, obscuring barcode recognition. Our specialists utilize precision optical lens cleansers and anti-static microfiber cleaning protocols to restore 100% optical clarity, followed by laser alignment audits to guarantee 99.5%+ read rates.
Motor Control Centers (MCC) & 480V Switchgear Restoration
Tunnel Motor Control Centers contain busbars, contactors, overload relays, and circuit breakers operating at 480 volts. Silt deposits create conductive tracking paths between phase conductors, resulting in catastrophic phase-to-phase short circuits if energized wet. Technicians utilize non-conductive CO2 dry ice blasting and dielectric solvent flushing to eliminate caliche residues without scratching plated bus surfaces, followed by 1,000V DC megohmmeter verification.
PLC Networks, Field Bus Cabling & Sensors
Industrial Ethernet, ControlNet, and AS-Interface (AS-i) sensor networks communicate critical bag tracking coordinates between sortation computers and diverter gates. Floodwater entering subterranean junction boxes corrodes RJ45 connectors and terminal blocks. We replace corroded modular termination blocks, execute Time Domain Reflectometry (TDR) cable integrity tests, and seal junction enclosures with IP67-rated waterproof gaskets.
Pneumatic Diverter Pushers & Solenoid Valves
High-speed sortation diverters rely on high-pressure pneumatic cylinders actuated by 24V DC solenoid valves to push bags onto designated airline sort spurs. Water intrusion through airline exhaust ports introduces abrasive caliche grit into cylinder bores, scoring Teflon seals and jamming valve spools. Technicians disassemble pneumatic manifolds, flush lines with clean instrument-grade dry compressed air, replace contaminated micro-filters, and re-lubricate cylinder barrels with aerospace-grade silicone lubricants.
Emergency Stop (E-Stop) Safety Circuit Verification
OSHA and FAA regulations require continuous failsafe operation of cable-pull emergency stop (E-stop) switches spanning the entire perimeter of subterranean conveyor lines. Silt and water ingress inside micro-switch contact blocks can bypass safety trip circuits or create false open-circuit faults that halt baggage sortation. Restoration technicians perform end-to-end loop resistance testing and mechanical contact burnishing across all E-stop stations, certifying 100% safety trip functionality before operational release.
When airport infrastructure experiences electrical equipment room flooding, facilities can consult our technical recovery protocols for data center water damage restoration for high-density server and electronic controller drying.
For commercial industrial properties facing large-scale mechanical plant flooding, see our capabilities for industrial warehouse water damage restoration.
Hyper-Local Phoenix Aviation Case Study: Sky Harbor Terminal 4 Baggage Tunnel Monsoon Flood
Emergency Subterranean Dewatering, Silt Slurry Extraction & Baggage Conveyor Desiccation
On a mid-August afternoon at 4:15 PM, an intense monsoon microburst centered over Phoenix Sky Harbor International Airport (3400 East Sky Harbor Boulevard, Phoenix, AZ 85034) dropped 2.35 inches of torrential rain within thirty-eight minutes. Runoff from the vast southern terminal apron breached the perimeter storm drainage swales adjacent to the Terminal 4 South Tug Drive Portal. Over 40,000 gallons of tarmac stormwater—carrying jet fuel residue, caliche clay, and tarmac debris—cascaded down the vehicular tug ramp into the below-grade baggage sortation tunnel. Water accumulated to a depth of thirty-eight inches in conveyor drive pits and low-level maintenance walkways, submerging thirty-two 480V conveyor drive motors, two vertical continuous lifts, and threatening four inline TSA explosive detection machines.
Baseline Conditions
Water Depth: 38 inches standing water
Ambient Tunnel: 92°F, 94% RH (192 GPP)
Concrete Subfloor: 99.9% WME (Saturated)
Affected Equipment: 32 drive motors, 4 EDS
Restoration Deployment
28-Minute Airside Response
2x 1,800 GPM Diesel Trash Pumps
1x 9,000 CFM Industrial Desiccant
24x Explosion-Proof Axial Blowers
Verified Results
Standing Water Cleared: 3.5 Hours
Relative Humidity Reduced to 24% RH
All 32 Motors Megohmmeter Cleared
Zero Cancelled Flights; Full Reopening in 34 Hrs
Commercial restoration director Marcus Vance and twenty-two SIDA-badged emergency technicians arrived on-site in twenty-eight minutes, escorted directly through Airfield Operations Area (AOA) Gate 14. Technicians deployed two 6-inch Godwin diesel trash pumps to evacuate the bulk floodwater to terminal pre-treatment interceptors within three and a half hours. Heavy truck-mounted vacuum units extracted over eighteen tons of caliche mud and silt from conveyor pit beds.
A trailer-mounted 9,000 CFM industrial desiccant dehumidifier was positioned on the airside service ramp, delivering dry process air down through tunnel stairwells. All thirty-two submerged conveyor drive motors were cleaned with dielectric wash, purged with dry air, and tested with Fluke 1587 megohmmeters, verifying insulation resistance greater than 65 megohms. In coordination with City of Phoenix Aviation Department engineers and TSA systems specialists, baggage handling operations were certified and fully restored thirty-four hours after the incident, completely avoiding multi-million-dollar airline diversion fees and passenger baggage loss claims.
Following mechanical restoration, our environmental team performed full ATP surface bioluminescence swab tests and airborne particulate monitoring across the entire tunnel envelope. Surface swab readings verified below 8 RLU, confirming total eradication of biological contaminants from tarmac bird refuse. Terminal engineering directors commended the rapid thirty-four-hour turnaround that preserved flight schedules during one of the busiest travel weekends of the summer season.
Aviation Authority Compliance, Airline Delay Claims & Insurance Transparency
Flooding within an airport terminal or subterranean baggage handling tunnel triggers intricate multi-party legal and financial liabilities. Stakeholders include municipal aviation departments (such as the City of Phoenix Aviation Department), airline operating consortiums, the FAA, TSA, and commercial property and business interruption insurance syndicates. Submitting claims for structural repair, equipment restoration, and extra expense reimbursement requires rigorous, audit-ready scientific documentation:
Aviation Insurance & Regulatory Documentation Deliverables
- OSHA Confined Space & Atmospheric Safety Logs: Complete time-stamped gas testing logs documenting oxygen, LEL, H2S, and CO levels across every work shift, ensuring total compliance with federal workplace safety standards.
- Itemized Xactimate Commercial Cost Estimates: Standardized commercial pricing breakdowns based on current Maricopa County industrial labor, equipment, and specialty remediation rates, recognized by major commercial insurers (AIG, Allianz, FM Global, Travelers).
- Certified Megohmmeter Electrical Clearance Reports: Individual testing certificates for all 480V electric motors, gearboxes, VFD drives, and MCC busbars documenting insulation resistance values before power re-energization.
- Daily Psychrometric Moisture Mapping: Comprehensive logs of ambient temperature, relative humidity, dew point, grains per pound (GPP), and substrate moisture content (WME) confirming scientific drying progress.
- FLIR Infrared Thermal Imaging Audits: High-resolution radiometric thermal images documenting moisture migration within below-grade concrete joints, elevator hoistways, and electrical raceways.
- Chain-of-Custody Hazardous Waste Disposal Manifests: Certified state and municipal EPA manifests documenting the extraction, transport, and permitted disposal of fuel-contaminated wastewater and caliche silt at licensed industrial waste handling facilities.
Consumer Protection & Commercial Insurance Billing Transparency
Valley Restoration Pros does not make misleading promises of "free deductible waivers" or claim that commercial property insurance will automatically cover 100% of restoration costs without facility responsibility. Commercial aviation coverage depends upon specific lease operating agreements, surface water flood endorsements, and deductible structures. We provide complete claims documentation assistance—furnishing daily psychrometric logs, ASTM concrete readings, thermal photography, and itemized billing sheets—to expedite swift, fair claim resolution with your insurance carrier.
Mandatory Commercial Restoration Guarantees
Valley Restoration Pros guarantees: Free Comprehensive On-Site Damage Assessment, Transparent Upfront Itemized Pricing Before Work Begins, and Assistance with Detailed Claims Documentation & Psychrometric Moisture Logs. We do not provide speculative telephone estimates; an on-site master restorer audits your aviation facility in person to deliver an exact, binding recovery plan.
For commercial airport facilities requiring immediate on-site damage assessment or emergency response, connect with our aviation dispatch team through our 24/7 commercial emergency operations center.
Frequently Asked Technical Questions: Subterranean Airport Baggage Tunnel Dewatering
Subterranean airport baggage tunnels flood because they sit below grade and are directly linked to surface airside aprons via sloped baggage tug drive ramps, conveyor intake portals, and utility shafts. Airfield ramps consist of vast expanses of impervious asphalt and concrete that produce massive sheet flow during intense monsoon downpours (often delivering over two inches per hour). When tarmac retention basins and oil-water interceptors exceed capacity, water flows down ramp portals into the tunnels. Furthermore, Phoenix caliche subsoil expands when saturated, exerting immense hydrostatic pressure that forces groundwater through concrete cold joints, seismic expansion seams, and electrical conduit penetrations.
Operations inside flooded subterranean airport tunnels comply with OSHA 29 CFR 1910.146 Permit-Required Confined Space standards. Before entry, certified safety supervisors complete atmospheric testing using calibrated 4-gas meters to verify safe oxygen levels (19.5%–23.5%), zero combustible hydrocarbon vapors (LEL < 10%), and absence of toxic gases like H2S and CO. Explosion-proof axial blowers provide continuous positive ventilation delivering at least 20 air changes per hour. Dedicated entry sentries maintain continuous visual and radio communication, and technicians wear safety harnesses connected to tripod retrieval systems at vertical access points.
Yes, provided power is locked out immediately before re-energization occurs and restoration begins within hours. Technicians disassemble motor end bells, flush stator windings with dielectric non-conductive solvents to dissolve silt and mineral deposits, and displace moisture using forced dry air. Gearbox lubricants are drained, flushed, and replaced with fresh synthetic oil. Variable frequency drives (VFDs) and electronic control boards are cleaned with specialized ultrasonic baths and dried in controlled low-humidity enclosures. Before re-energizing, certified technicians perform 1,000V DC insulation resistance testing with digital megohmmeters; windings verifying greater than 50 megohms are successfully returned to service without expensive replacement.
Airport apron stormwater is classified as Category 3 blackwater. It contains unburned Jet-A aviation fuel, hydraulic fluids (synthetic ester and phosphate fluids), glycol deicing residues, aircraft tire rubber particulates, avian droppings carrying biological pathogens, and abrasive dissolved caliche minerals (calcium carbonate and silica). Neutralization requires closed-loop thermal extraction using softened demineralized water heated to 200°F combined with EPA-registered hydrocarbon emulsifiers and broad-spectrum antimicrobial sanitizers to digest organic residues and eliminate biological pathogens without corroding steel conveyor mechanisms.
In subterranean concrete tunnels, cooler wall and ceiling surfaces create a continuous condensation trap when high-humidity air is present. Standard refrigerant dehumidifiers fail in hot, low-grain environments. Large industrial desiccant dehumidifiers utilize silica gel chemical wheels that continuously adsorb water vapor from the tunnel air, lowering the dew point to below 35°F and reducing humidity ratios to under 20 grains per pound (GPP). By maintaining the tunnel dew point substantially lower than surface concrete and steel temperatures, condensation is physically prevented from forming, eliminating moisture dripping onto conveyor belts and electrical switchgear.
Valley Restoration Pros maintains an emergency response division whose supervisors hold active SIDA (Security Identification Display Area) badging for commercial airport facilities. For large-scale events requiring multiple crews, our dispatch center coordinates directly with TSA Federal Security Directors and Airport Police to establish designated secure escort corridors through Airfield Operations Area (AOA) perimeter gates. All dewatering equipment, recovery vehicles, and tooling undergo rapid pre-clearance inspections, ensuring continuous 24/7 restoration operations proceed without compromising airport security standards.
Valley-Wide Aviation Rapid Response Corridors: 30-Minute Commercial Airport Dispatch
Subterranean airport baggage handling tunnel flooding demands instantaneous mobilization by certified master commercial restorers possessing self-contained industrial pumping assets and low-grain desiccant fleets. Valley Restoration Pros maintains dedicated emergency aviation teams positioned strategically across Maricopa County, guaranteeing on-site arrival within thirty minutes:
Phoenix Sky Harbor International Airport (PHX) & Downtown Hub
Providing immediate 24/7 priority response for Terminal 3, Terminal 4, and subterranean air cargo transfer tunnels along Buckeye Road and Sky Harbor Boulevard. Connect with our dedicated Phoenix commercial airport dewatering emergency dispatch team.
Phoenix-Mesa Gateway Airport (AZA) & East Valley Aerospace Hub
Serving commercial passenger terminals, flight training academies, and aerospace maintenance facilities across Sossaman Road and Ray Road. Mobilize our specialized Mesa aviation facility flood recovery division.
Scottsdale Airport (SDL) & Corporate Aviation Airpark
Delivering high-capacity extraction and desiccant drying for executive corporate hangars, private jet terminals, and avionics repair vaults along Airport Drive. Contact our Scottsdale commercial airpark restoration squad.
Tempe Tech Basin & Aviation Logistics Corridors
Providing high-velocity extraction and dehumidification for air freight forwarders, ground logistics hubs, and aerospace research centers along University Drive and Rio Salado Parkway. Access our Tempe aviation logistics dewatering team.
Glendale Municipal Airport (GEU) & West Valley Aerospace
Delivering 24/7 confined space extraction and structural drying for aviation manufacturing plants and flight test facilities in Glendale and Peoria. Mobilize our Glendale aviation structural recovery unit.
Chandler Municipal Airport (CHD) & Price Tech Corridor
Providing precision electronics desiccation and subterranean dewatering for avionics research laboratories and aircraft maintenance complexes. Connect with our Chandler aerospace facility restoration specialists.
Deer Valley Airport (DVT) & North Phoenix Aviation Corridor
Supporting one of the nation's busiest general aviation and pilot training flight centers along Deer Valley Road. Deploy our specialized industrial emergency water extraction and desiccation units for hangars and support vaults.
Master Valley-Wide Aviation Emergency Response
For centralized emergency dispatch across all municipal, commercial, and military airfield operations in Maricopa County, explore our comprehensive Valley-wide commercial restoration coverage directory.
When monsoon stormwater or subterranean hydro-static pressure inundates your airport baggage handling tunnels, every minute of operational downtime multiplies flight delays, baggage misdirection claims, and electrical equipment destruction. Contact commercial aviation restoration director Marcus Vance immediately at (602) 847-9593 for certified 24/7 emergency response.
Verified Local Area Dispatch: Phoenix, AZ
Official Geo-Coordinates: 33.4484° N, -112.074° W • Maricopa County
Related Specialized Emergency Restoration Services
Explore specialized rapid-response mitigation protocols across Greater Phoenix and Maricopa County:
Valley-Wide Emergency Response Service Coverage
Our mobile restoration fleet is dispatched across the entire Phoenix metropolitan region, providing rapid 30 to 60 minute emergency response: