
Valley Restoration Pros delivers 24/7 industrial emergency water extraction, thermal psychrometric drying, and structural mitigation across Phoenix and Maricopa County with guaranteed 30–60 minute rapid arrival. All protocols strictly adhere to IICRC S500 standards, featuring upfront itemized pricing and free on-site thermal moisture assessments. Call dispatch directly at (602) 847-9593.
Why Immediate Mitigation Is Critical in Phoenix Heat
Sub-fab process cooling water (PCW) and ultra-pure water (UPW) line bursts discharge thousands of gallons per minute beneath vibrating cleanroom waffle slabs, threatening high-voltage dry vacuum pumps and transformer substations. Chandler municipal groundwater and industrial supply lines carry 18 to 25 grains per gallon (GPG) of dissolved calcium and magnesium minerals, leaving conductive electrolytic deposits across sensitive robotic plinths. Under Chandler 115°F summer heat, sub-fab utility crawlspaces rapidly exceed 90% relative humidity, triggering runaway fungal incubation and secondary airborne particulate blooms within 24 to 48 hours. Liquid pooling around chemical delivery systems (CDS) risks mobilizing hazardous production materials (HPM), demanding immediate SEMI S2 containment and hazardous gas monitoring isolation.

Service Definition & The IICRC Standard of Care
Professional price corridor commercial sub fab water damage restoration chandler is an engineering and environmental discipline adhering strictly to IICRC S500 protocols, not mere surface mopping. When structural plumbing failures strike in Maricopa County, certified emergency water extraction and thermal structural drying procedures must be deployed immediately. Whether triggered by high-pressure burst pipe emergencies, subfloor leaks, or commercial line ruptures, bound moisture rapidly penetrates concrete subfloors and wall framing. In the desert heat, delays trigger microbial proliferation requiring rapid mold remediation. Request damage assessment through our emergency assessment portal or request 30-minute dispatch across all Valley service areas.
Securing electrical feeds, inspecting load-bearing assemblies, and containing pathogens.
Stopping the intrusion source and erecting 6-mil plastic isolation containment airlocks.
31-HP truck-mount extraction, removing gallons exponentially faster than evaporation.
LGR dehumidifiers and HEPA air scrubbers driving grains per pound below 25 GPP.
Calibrated electronic pinless testing confirming baseline dry standards.
The Complete 6-Stage Restoration Roadmap
Our IICRC-certified crews execute a disciplined, scientific 6-stage protocol to stabilize and dry structural components:
Emergency Dispatch & Perimeter Isolation
30 to 60 minute arrival. Securing electrical shutoffs, evaluating structural loads, and erecting containment airlocks.
FLIR® Thermal Mapping & Baseline Scans
Infrared thermal scans detect trapped moisture behind walls and beneath concrete without invasive exploratory demolition.
High-Volume Bulk Extraction
31-HP truck-mount extraction units pump standing water away at hundreds of gallons per minute.
Controlled Selective Demolition
Precision flood cuts 12 to 24 inches above moisture lines, removing wet insulation and opening wall framing to dry airflow.
Thermodynamic Dehumidification
Industrial Low-Grain Refrigerant dehumidifiers pull deep trapped moisture from dense framing lumber and concrete slabs.
Antimicrobial Sanitization & Verification
EPA-registered botanical application (Benefect Decon 30) and calibrated moisture testing to issue an official dry certificate.
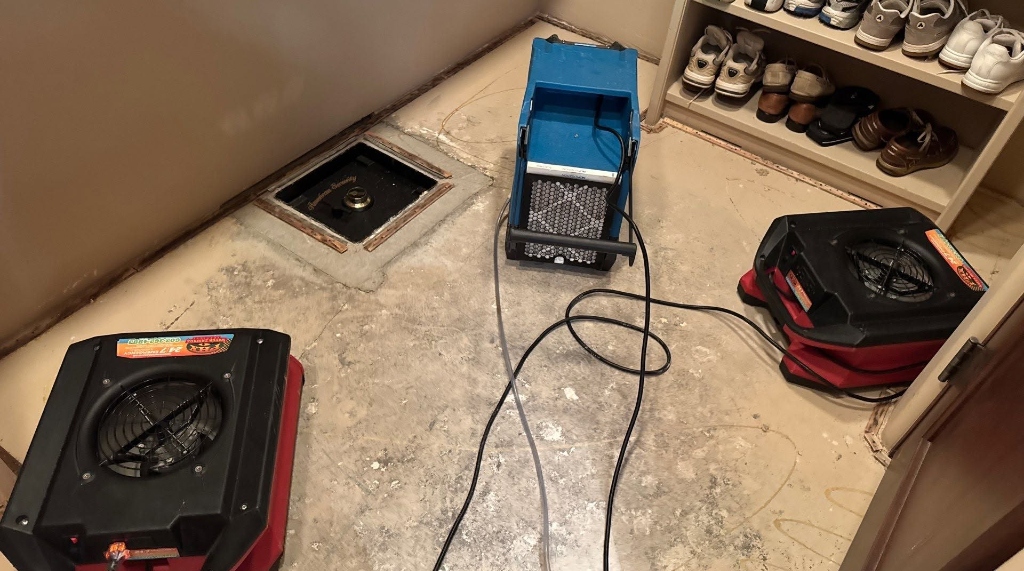

Specialized Equipment & Industrial Restoration Technology
Mitigating severe property damage requires industrial-grade technology capable of altering thermodynamic psychrometrics:
Truck-Mounted Extraction Rigs
31-HP engines producing 16+ inches Hg vacuum suction to evacuate bulk water rapidly into holding tanks.
Low-Grain Refrigerant Dryers
Pre-cooling heat-pipe systems driving ambient grains per pound below 25 GPP to draw deep trapped water out of framing.
HEPA Negative-Air Scrubbers
Hospital-grade 99.97% particulate filtration capturing microscopic fungal spores, soot, and biohazard aerosols.
FLIR® Thermal Scanners & Probes
Infrared thermography detecting evaporative cooling boundaries behind walls, combined with digital RF pinless scanners.
Professional Restoration vs. DIY Mitigation
Attempting DIY cleanup during a property disaster creates severe hidden liabilities:
- Trapped Moisture: Surface drywall dries while moisture inside cavities triggers hidden mold blooms.
- Pathogenic Risks: Category 2 & 3 water contains bio-contaminants standard cleaners fail to kill.
- Insurance Denial: Insurers require daily psychrometric logs; lack of data causes claim disputes.
Transparent Upfront Itemized Pricing
Valley Restoration Pros operates with complete transparency:
- Free On-Site Assessment: Complete physical inspection before work begins.
- Upfront Itemized Estimates: Detailed line items calculated via industry-standard Xactimate.
- Zero Surprise Billing: No hidden charges or unauthorized repairs.
Certified Price Corridor commercial sub fab water damage restoration Chandler Field Documentation
Every response performed by Valley Restoration Pros is documented through photographic and thermographic records:

Comprehensive Price Corridor commercial sub fab water damage restoration Chandler Technical Manual & Operational Standards
Exhaustive engineering protocols, psychrometric calculations, geological multipliers, and step-by-step restoration standards for Maricopa County properties:
Executive Emergency Abstract: Price Corridor Semiconductor Sub-Fab Utility Inundation & Critical Cleanroom Recovery
The Price Road Corridor in Chandler, Arizona, represents one of the most technologically advanced microelectronics and semiconductor manufacturing epicenters in the world. Encompassing major mega-fab facilities and production campuses such as the Intel Ocotillo Campus, NXP Semiconductors, and Microchip Technology along the Price Road, Dobson Road, and Queen Creek Road industrial corridors, these multi-billion-dollar fabrication ecosystems operate continuously under sub-nanometer tolerances. Beneath every state-of-the-art cleanroom floor lies an equally massive, ultra-complex sub-fab utility basement: a subterranean mechanical level housing continuous closed-loop Process Cooling Water (PCW) mains, Ultra-Pure Water (UPW) polishing loops, high-voltage dry vacuum backing pump arrays, chemical dispensing systems, toxic gas abatement scrubbers, and primary power substations.
When a mechanical failure occurs—such as an 8-inch high-pressure PCW distribution manifold flange shear, a chemical-resistant UPW loop joint failure, an acid waste line hydraulic backup, or an accidental fire protection pre-action deluge discharge—the sub-fab basement becomes the site of an operational crisis. Thousands of gallons of pressurized industrial process water cascade across reinforced concrete foundation slabs, submerging subterranean utility trenches and rising toward sensitive electrical switchgear. Unlike ordinary commercial warehouse flooding, an inundation inside an advanced semiconductor sub-fab threatens millions of dollars per hour in cleanroom stoppage, risks irreversible vapor-phase contamination of Class 1 cleanroom environments directly overhead, and creates severe electrical and hazardous chemical exposure risks.
Rapid deployment of specialized industrial emergency water extraction is required within sixty minutes of initial breach detection. Sub-fab environments are not passive basements; they are dynamic, negative-pressure aerodynamic chambers coupled to cleanroom air recirculating pathways. Moisture left standing on concrete slabs rapidly evaporates into return air plenums, driving relative humidity above the strict 35 to 45 percent threshold mandated by cleanroom environmental standards. The resulting moisture condensation on optical photolithography steppers, extreme ultraviolet (EUV) mirrors, wafer transport tracks, and electrostatic chucks can ruin entire production runs of work-in-progress silicon wafers.
Immediate Sub-Fab Emergency Directives: First 30 Minutes
- Initiate Automated SCADA Loop Isolation: Immediately trip automated supervisory isolation valves on affected PCW or UPW supply headers to halt volumetric discharge while maintaining secondary chilled water loops to operating production tooling.
- De-Energize Sub-Fab Floor Power Transformers: Coordinate with facility electrical engineering to isolate 480V 3-phase secondary distribution substations and busways feeding sub-fab vacuum pump arrays to prevent catastrophic arc flash and electrocution hazards in flooded trenches.
- Confirm Toxic Gas & Chemical Interlocks: Verify that Toxic Gas Monitoring Systems (TGMS) and chemical delivery emergency shutoff valves (ESVs) have automatically isolated hazardous production material lines passing through the flooded utility chase.
- Mobilize Industrial Semiconductor Restoration Teams: Contact Valley Restoration Pros directly at (602) 847-9593 or tap Emergency Phone Dispatch for immediate on-site response along the Chandler Price Corridor.
Anatomy of Sub-Fab Utility Inundation & Cleanroom Plinth Water Dynamics
A semiconductor manufacturing plant represents an inverted structural hierarchy. Above sits the ultra-clean ballroom fabrication space, where automated material handling systems (AMHS) glide along ceiling monorails transferring 300mm wafer front-opening unified pods (FOUPs) between multi-million-dollar photolithography tracks, chemical mechanical planarization (CMP) stations, and reactive ion etching chambers. Supporting this immaculate cleanroom floor is a heavily reinforced post-tensioned concrete waffle slab perforated by thousands of circular openings that allow laminar airflow to sweep downward through raised metal pedestal floor tiles.
Directly beneath this waffle slab sits the sub-fab, typically a subterranean or semi-subterranean concrete chamber with clear heights ranging from 15 to 25 feet. The sub-fab serves as the mechanical engine room for the cleanroom above. Precision process tools are anchored directly to structural concrete plinths or structural steel grillage that penetrate through the raised floor directly to the sub-fab structural slab. Connected to the underside of these production tools are hundreds of feed and return utility conduits: high-purity perfluoroalkoxy (PFA) and polyvinylidene fluoride (PVDF) lines carrying ultra-pure water, stainless steel lines circulating process cooling water, fluoropolymer-lined acid exhaust ducts, slurry supply loops, and high-vacuum forelines.
When catastrophic water releases occur in a semiconductor facility, the hydrodynamics behave differently than in typical commercial water damage scenarios. Process cooling water systems operate under continuous hydraulic pressures between 60 and 90 pounds per square inch (PSI), with volumetric flow rates exceeding 1,200 gallons per minute per distribution loop. A sudden mechanical shear or elastomeric gasket blow-out on an 8-inch stainless header results in an explosive hydrodynamic release that floods hundreds of square feet within seconds. High-pressure water jets strike overhead cable raceways, structural vibration pedestals, and dry vacuum pump skids before cascading onto the monolithic concrete floor.
Because the sub-fab floor is engineered with drainage slope gradients leading toward chemical collection sumps and acid waste neutralization (AWN) lift stations, standing water quickly cascades toward sunken utility trenches. As water depth surpasses two inches, high-voltage dry vacuum backing pumps, turbomolecular pump controllers, and radio-frequency (RF) power generators anchored to equipment plinths become partially submerged. Even non-corrosive water creates catastrophic electrolytic bridging across terminal junction boxes, initiating electrical short-circuits and frying expensive electronic assemblies.
Simultaneously, unexpected hydraulic pressure waves can trigger a secondary burst pipe repair emergency on adjacent pneumatic or ultrapure lines. When high-velocity fluid strikes structural vibration-isolation pedestals, it transmits kinetic energy throughout the structural grillage. Cleanroom steppers performing sub-nanometer extreme ultraviolet (EUV) lithography depend on absolute vibrational isolation; physical water impact and hydrostatic buoyancy forces acting on tool plinths can knock optical assemblies out of alignment, causing weeks of recalibration delays and multi-million-dollar yield losses.
Capillary action also presents a grave threat across concrete plinths. Reinforced concrete is naturally porous, containing interconnected capillary networks. When standing water remains ponded around plinth bases, water wicks upward through the concrete matrix toward tool baseplates. This moisture migration elevates localized relative humidity within tool internal enclosures, triggering microscopic dendritic growth on circuit boards and degrading sensitive vibration damping elastomeric isolators.
Critical Sub-Fab Infrastructure Vulnerability Matrix
| Component | Operating Environment | Inundation Threat Level | Direct Failure Mechanism |
|---|---|---|---|
| Dry Vacuum Backing Pumps | Sub-fab floor plinths | Critical | Motor housing flooding, stator short-circuit, seal corrosion |
| RF Power Generators | Plinth rack mountings | Critical | High-voltage transformer grounding, dielectric flashover |
| Laminar Recirculation Plenums | Vertical air shafts | High | Moisture vapor aspiration, cleanroom humidity elevation |
| Waffle Slab Post-Tension Anchors | Reinforced overhead slab | Moderate | Micro-fracture moisture retention, long-term tendon corrosion |
Chandler & Sonoran Desert Environmental Multipliers
Performing commercial disaster restoration within the Chandler technology manufacturing corridor requires a deep technical comprehension of the unique geological, environmental, and municipal conditions characterizing the East Valley of Greater Phoenix. While semiconductor production cleanrooms maintain rigorously controlled indoor micro-climates, sub-fab mechanical basements, deep foundation footings, and incoming raw utility feeds are directly influenced by the unforgiving Sonoran Desert environment.
A primary environmental stressor in Chandler water damage emergencies is the extreme chemical profile of local municipal water supplies. Derived from Salt River Project (SRP) surface reservoirs, Central Arizona Project (CAP) Colorado River allocations, and regional deep groundwater aquifers, Chandler water exhibits extreme hardness ranging from 18 to over 25 Grains Per Gallon (GPG), equivalent to 300 to 425+ parts per million (PPM) of total dissolved solids (TDS). High concentrations of dissolved calcium bicarbonate, magnesium sulfate, and silicates flow through raw industrial feed lines and fire deluge systems.
When an unpurified raw industrial water line, chiller loop, or fire protection deluge riser ruptures inside a sub-fab, the standing liquid carries this severe mineral charge. As standing water evaporates in the high-heat, high-airflow sub-fab environment, it leaves behind a stubborn crust of chalky, conductive mineral scale across equipment skids, terminal wiring blocks, and polished stainless steel conduits. These crystalline scale formations harbor microscopic hygroscopic salts that continually attract ambient moisture from the air, promoting galvanic pitting corrosion on electrical contacts and vacuum pump flanges long after bulk standing water has been removed.
A second major local multiplier is the geology beneath the Price Road Corridor. The Chandler basin consists of deep alluvial sediments interbedded with dense caliche horizons—cemented calcium carbonate strata that act as impervious subterranean barriers. During periods of heavy municipal irrigation or seasonal monsoon storms, moisture cannot easily drain downward into deep aquifers. Instead, water trapped beneath concrete slabs creates hydrostatic uplift pressures. If an undetected under-slab process line fails, water migrates horizontally along the caliche interface, elevating moisture vapor emission rates (MVER) through the sub-fab foundation slab. Resolving this subterranean saturation demands specialized slab leak water damage restoration procedures engineered specifically for industrial post-tension foundation slabs.
Expansive clay soils commonly found in Chandler also pose structural risks. When subjected to wetting from major utility line ruptures, native smectite and bentonite clay minerals expand by up to 10 to 15 percent by volume. This localized soil heave exerts differential uplift forces against deep concrete caissons and perimeter footing walls. In a facility where lithography equipment requires floor stability down to sub-micron vibrational criteria, even minute soil movements can distort machine calibrations and demand expensive geotechnical remediation.
Finally, Chandler ambient summer temperatures regularly reach 112°F to 118°F from June through September. During a major utility pipe rupture, sub-fab exhaust systems may be disrupted or throttled. Under these high ambient temperatures, stagnant water pools inside unconditioned utility chases turn into accelerated biological incubators. Psychrometric microbial kinetics dictate that mold spore germination and fungal mycelial growth accelerate exponentially above 85°F with relative humidity exceeding 70 percent. Within 24 to 48 hours, unmitigated sub-fab standing water risks spawning systemic fungal contamination, requiring intensive industrial mold remediation under negative pressure containment to protect the cleanroom overhead.
Sonoran Desert Industrial Hazard Warning
Never allow sub-fab standing water to air-dry naturally under Chandler summer conditions. Accelerated evaporation deposits thick silicate scale that bonds chemically with electronic contacts, while the thermal multiplier turns damp sub-grade concrete into an aggressive fungal breeding ground within 36 hours. Immediate commercial extraction and desiccant psychrometric dehumidification are essential.
First-Hour Sub-Fab Hazmat Isolation & Chemical Valve Interlocks
The initial sixty minutes following a sub-fab liquid breach are critical in determining whether an incident remains an isolated utility spill or escalates into a catastrophic multi-million-dollar hazardous materials event. In a semiconductor fabrication facility, sub-fab basements do not merely house clean cooling water; they are co-located alongside high-risk chemical delivery systems (CDS) distributing concentrated acids, volatile solvents, caustic bases, and pyrophoric gases.
Standard emergency water response procedures are wholly inadequate in a sub-fab environment. Before any vacuum hose is uncoiled or any extraction technician enters the subterranean space, facility managers and responding teams must execute a synchronized hazardous material isolation sequence. Chemical lines carrying hydrofluoric acid (HF), sulfuric acid (H2SO4), ammonium hydroxide (NH4OH), and hydrogen peroxide (H2O2) often traverse the very trenches now filling with water. If rising water contacts unrated electrical connections on chemical pump skids, or if hydrostatic pressure shifts chemical transport tubing, severe chemical leaks can occur simultaneously.
In facilities with dedicated below-grade neutralization tanks, responding teams must immediately verify the operational integrity of lift stations. When an overflow occurs involving chemical trenches, specialized commercial semiconductor acid waste neutralization pit flood protocols must be integrated into the response. Portable electrochemical sensors and multi-gas photoionization detectors (PIDs) must continuously monitor the sub-fab atmosphere for volatile organic compounds (VOCs), acidic vapor mists, and hazardous gas releases before work crews enter.
Electrical safety is paramount during this initial hour. Sub-fab spaces are energized by heavy 480V 3-phase industrial power busses routing through overhead cable trays, floor-mounted busways, and transformer cabinets. Water spraying from a high-pressure line burst can pool on top of busway enclosures, creating severe flashover hazards. Responding emergency personnel must coordinate with plant electrical engineers to execute Lockout/Tagout (LOTO) procedures on all non-essential electrical distribution panels feeding the impacted quadrant while preserving essential cleanroom ventilation and toxic gas exhaust systems.
Technicians mobilized by Valley Restoration Pros arrive equipped with specialized Level B and Level C personal protective equipment (PPE), including chemical-resistant boots, vapor-tight respirators, and intrinsically safe diagnostic meters. Air quality is verified using multi-gas sniffers testing for oxygen deficiency, lower explosive limit (LEL), carbon monoxide, hydrogen sulfide, and chlorine vapors. To initiate rapid staging or coordinate with our Chandler industrial rapid response team, facility directors can immediately contact us for round-the-clock commercial emergency dispatch.
Sub-Fab Hazmat First-Hour Checklist
- Execute automated or manual emergency shutoff valve (ESV) closure on all chemical delivery lines traversing the flooded utility sector.
- Verify zero alarms on the Toxic Gas Monitoring System (TGMS) console and confirm continuous negative-pressure draft on scrubbed chemical exhaust ducts.
- Perform pH strip and electrochemical dip-probe testing of standing water in utility trenches to confirm neutral fluid (pH 6.5 - 7.5) before mechanical pumping.
- Establish Lockout/Tagout (LOTO) boundaries on all flooded 480V distribution panels, motor control centers, and dry vacuum pump circuits.
- Establish restricted-entry hot, warm, and cold decontamination zones at all sub-fab stairwells and equipment access hatches.
Advanced Industrial Cleanroom Extraction & Desiccant Drying Infrastructure
Remediating water disasters in advanced technology manufacturing environments demands industrial-scale equipment configurations that far exceed typical commercial restoration assets. Because sub-fab basements are interconnected with cleanroom recirculating air plenums, the extraction and dehumidification systems deployed must not introduce any particulate contaminants, airborne oil vapors, or uncontrolled thermal spikes into the facility envelope.
Valley Restoration Pros maintains a fleet of heavy-duty, self-contained extraction and drying assets engineered specifically for high-tech cleanroom and sub-fab environments along the Chandler Price Corridor. For rapid bulk water removal across extensive concrete floor areas and subterranean trenches, our teams utilize trailer-mounted, positive-displacement vacuum extraction plants. Capable of moving over 1,500 gallons per minute through 4-inch crush-proof vacuum hoses, these units rapidly dewater deep utility vaults without venting exhaust gases inside the plant. For areas adjacent to sensitive electronic equipment, we deploy explosion-proof, pneumatically driven diaphragm pumps that operate with zero electrical spark risk and zero electromagnetic interference (EMI).
Once bulk liquid water has been thoroughly removed from floor slabs, sumps, and trenches, the critical phase of industrial structural drying begins. Traditional refrigerant dehumidifiers (such as standard LGR units) are often insufficient in cleanroom facilities because they struggle to pull relative humidity below 35 percent, particularly in conditioned sub-fab spaces with low ambient temperatures. Cleanrooms require deep psychrometric drying conditions where the dew point is forced below 30°F and specific humidity drops below 25 Grains Per Pound (GPP).
To achieve this rigorous standard, Valley Restoration Pros deploys commercial desiccant dehumidifiers ranging from 5,000 to 15,000 CFM (cubic feet per minute). Powered by external diesel generators staged outside the facility perimeter, these trailer-mounted desiccant systems utilize synthetic silica gel sorption rotors. They process incoming humid air and deliver ultra-dry supply air at less than 10 percent relative humidity and sub-zero dew points. Clean lay-flat ducting is routed through dedicated exterior utility pass-through ports into the sub-fab basement, flooding the flooded bays with ultra-dry air while exhausting reactivation air safely outside the building envelope.
This deep desiccant drying technology is especially vital when protecting delicate mission-critical equipment, mirroring the psychrometric controls used in our data center server room water damage mitigation procedures. Concrete foundation slabs in semiconductor facilities are typically 18 to 36 inches thick to dampen external vibrations. Once saturated by thousands of gallons of water, these massive concrete masses retain vast reservoirs of bound moisture. Without continuous desiccant dehumidification creating a steep vapor pressure gradient across the slab surface, moisture will slowly off-gas over several months, blistering epoxy floor sealants and raising cleanroom ambient humidity.
Furthermore, air movement within the sub-fab must be carefully controlled. Standard high-velocity centrifugal air blowers can lift dust particles and aerosolize mineral scale deposits into ambient air streams, where they might enter return air plenums. Valley Restoration Pros utilizes variable-speed, laminar-airflow air movers paired with in-line HEPA air filtration scrubbers rated at 99.97 percent efficiency down to 0.3 microns. By maintaining a clean, controlled drying chamber beneath the waffle slab, we ensure that the cleanroom overhead remains uncompromised throughout the drying process.
In addition to air scrubbing, our teams deploy continuous aerosol particle monitors (laser optical particle counters) calibrated to ISO 14644-1 Cleanroom Standards. These instruments log airborne particulate counts in real time, alerting technicians immediately if physical demolition or equipment movement generates particulate spikes above acceptable baseline thresholds. This continuous particulate monitoring provides verifiable documentation that cleanroom air purity has been preserved throughout the entire structural drying cycle.
Thermal control during drying is equally critical. Desiccant reactivation exhausts substantial thermal energy, which must never be allowed to heat the structural slab beneath sensitive metrology equipment. By placing desiccant reactivators outside the building envelope and introducing tempered dry air through insulated supply trunklines, we ensure that sub-fab ambient temperatures remain stable between 68°F and 72°F, avoiding thermal expansion of precision equipment mounting plinths.
Industrial Sub-Fab Drying Equipment Specifications
| Equipment Type | Capacity / Rating | Operating Metric | Cleanroom Sub-Fab Purpose |
|---|---|---|---|
| Trailer Desiccant Dehumidifiers | 5,000 - 15,000 CFM | <10% RH, <20 GPP supply | Deep concrete slab moisture extraction & dew point depression |
| Pneumatic Diaphragm Pumps | 150 - 300 GPM per unit | Air-driven, ATEX rated | Explosion-proof fluid extraction from utility trenches & sumps |
| HEPA Air Scrubbers (DOP Tested) | 2,000 CFM per unit | 99.97% @ 0.3 microns | Particulate capture & negative pressure containment isolation |
| High-Pressure Extraction Wands | 1,200 PSI / continuous vac | Closed-loop recovery | Concrete surface decontamination and mineral residue flushing |
IICRC S500 / S520 Restoration Protocol Step-by-Step
To ensure absolute rigor and full audit compliance for semiconductor property owners, commercial insurance underwriters, and facility compliance engineers, Valley Restoration Pros executes a specialized six-stage restoration protocol. This framework synthesizes the standards of the Institute of Inspection, Cleaning and Restoration Certification (IICRC S500 Standard for Professional Water Damage Restoration and S520 Standard for Professional Mold Remediation) with stringent semiconductor cleanliness specifications, similar to our comprehensive semiconductor cleanroom water damage restoration phoenix procedures.
Stage 1: Psychrometric Baseline Diagnostics & Hazard Stratification
Upon arrival, Master Certified Restoration Technicians immediately deploy digital thermo-hygrometers, laser surface thermometers, and high-resolution thermal imaging cameras (FLIR T-Series) to map thermal gradients, dew points, and vapor pressure differentials across the sub-fab. Baseline psychrometric conditions are documented, logging ambient dry-bulb temperature, relative humidity, Grains Per Pound (GPP), and vapor pressure in inches of mercury (inHg). Moisture readings within structural concrete slabs, plinth footings, and structural steel supports are logged using pinless radio-frequency meters and calibrated electrical impedance sensors. Liquid samples are collected from flooded trenches to stratify the water category: Category 1 (clean process cooling water or pure condensate), Category 2 (process water mixed with chemical surfactants or mineral scale), or Category 3 (sewage backflow or chemical contamination requiring full sewage cleanup and biohazard sanitization protocols).
Detailed thermal imaging also identifies sub-surface moisture migration within equipment pedestal footings and vibration isolation mounts. Moisture trapped beneath heavy equipment baseplates emits distinct thermal signatures that direct targeted suction drying, eliminating guesswork and ensuring zero hidden moisture pockets remain unnoticed.
Stage 2: Critical Barrier Containment & Airflow Isolation
To isolate the sub-fab atmosphere from cleanroom recirculating air handlers, our crew constructs heavy 6-mil flame-retardant anti-static polyethylene isolation barriers across all access shafts, waffle slab penetrations, and vertical utility raceways. Differential pressure manometers are installed to monitor and maintain continuous negative air pressure (-0.02 to -0.04 inches of water column) within the affected sub-fab zone relative to the cleanroom above. This prevents humid air, evaporated mineral aerosols, or disturbed particulate matter from migrating into Class 100 or Class 1 cleanroom areas.
Airlocks with triple-chamber decontamination enclosures are installed at primary personnel ingress and egress portals. Technicians transition through clean ante-rooms, donning lint-free cleanroom coveralls, shoe covers, and electrostatic-discharge (ESD) grounding straps before entering sensitive sectors.
Stage 3: High-Volume Industrial Fluid Extraction & Trench Sump Pumping
Technicians deploy heavy extraction arrays, utilizing positive displacement vacuum systems and non-sparking pneumatic pumps to evacuate standing water from foundation slabs, subterranean drainage trenches, elevator pits, and pipe chases. Water extraction is performed systematically, working from the highest structural elevation down to lowest sump pits. Rubber-squeegee vacuum wands and enclosed surface extractors recover standing water without generating liquid splashing or airborne droplet mists that could compromise nearby electrical gear.
Specialized low-clearance extraction tools are directed into tight utility chases beneath cable trays and process piping, extracting water pooled in narrow expansion joints and floor depressions where automated drainage systems cannot reach.
Stage 4: Decontamination, Scale Neutralization & Vacuum Surface Flushing
Because Chandler municipal and industrial water supplies carry heavy mineral burdens (18 to 25 GPG), removing standing water is only half the battle. Evaporation leaves conductive mineral films and scale deposits across equipment housings and concrete floors. Technicians apply non-conductive, residue-free specialized cleaning agents to dissolve calcium, magnesium, and silica scale. Surfaces are wiped down and rinsed using closed-loop hot-water extraction tools with zero wastewater escape. If biological or fungal amplification is identified, EPA-registered, cleanroom-compatible botanical antimicrobials are applied to neutralize spores without leaving volatile chemical residues.
All recovered rinse water is collected in dedicated hazmat drums or pumped to approved on-site industrial wastewater treatment systems following strict plant environmental protocols.
Stage 5: Industrial Desiccant Psychrometric Stabilization
With all standing liquid eliminated and surfaces cleaned, large-capacity trailer desiccant dehumidifiers (5,000 to 15,000 CFM) are engaged. Ultra-dry air (sub-zero dew point, <10% RH, <20 GPP) is ducted directly into the sub-fab containment zone. Axial and laminar air movers circulate this dry air across concrete slabs, plinth structural pedestals, and under-floor cable raceways, establishing a continuous vapor pressure gradient that draws bound moisture out of porous concrete structures. Psychrometric parameters (temperature, RH, dew point, GPP, and vapor pressure) are recorded every two hours in computerized moisture logs to track drying progress against established dry standards.
Vapor pressure differentials are strictly controlled to prevent concrete thermal shock while maximizing water molecule desorptive release from deep slab capillary pores.
Stage 6: Non-Destructive Testing, Laser Metrology & Final Sign-Off
Prior to demobilizing drying equipment and restoring full production operations, rigorous verification protocols are executed. In-situ relative humidity probes (ASTM F2170) embedded within concrete slabs must confirm slab internal moisture levels below 75 percent RH. Laser interferometry and precision dial indicators measure tool plinth elevation to verify that zero foundation subsidence or soil expansion has occurred. Airborne particulate counts are verified via laser particle counters to confirm compliance with ISO 14644-1 cleanroom classifications. Only when all environmental, structural, and mechanical parameters return to verified baseline standards is the restoration zone certified ready for full operational handoff.
A comprehensive completion dossier is compiled, including signed moisture logs, thermal certification images, air particulate test sheets, and structural level surveys for commercial insurance subrogation and corporate EHS compliance files.
SEMI S2 Environmental Safety & OSHA Hazardous Production Materials (HPM) Compliance
Industrial emergency disaster restoration within an active semiconductor fabrication environment requires strict compliance with international manufacturing safety directives. Unlike standard commercial buildings governed purely by local municipal building codes, semiconductor plants are subject to SEMI S2 (Environmental, Health, and Safety Standard for Semiconductor Manufacturing Equipment) and OSHA 29 CFR 1910.119 (Process Safety Management of Highly Hazardous Chemicals).
When water inundates sub-fab utility chases, it intersects directly with systems classified under the International Fire Code (IFC) and NFPA 318 as Hazardous Production Material (HPM) facilities. HPM regulations mandate that all secondary chemical containment piping, spill drainage troughs, and leak detection sensors remain fully functional at all times. Valley Restoration Pros coordinates directly with facility Environmental Health and Safety (EHS) officers to ensure that our emergency extraction actions never compromise active safety interlocks, spill sensors, or chemical exhaust pathways.
SEMI S2 mandates specific criteria for electrical equipment enclosures and mechanical interlocks during emergency interventions. Restoration equipment introduced into the sub-fab must be rated to prevent sparking in potentially flammable vapor atmospheres and must adhere to cleanroom contamination controls. Any water extraction around closed-loop chiller circuits must also follow standards established in our commercial chiller pipe flood restoration protocols to avoid disturbing high-pressure chemical glycol blends or refrigerant lines.
All technicians entering the sub-fab hold active OSHA 40-hour HAZWOPER certifications, cleanroom protocol badges, and confined space entry credentials. Continuous atmospheric air monitoring for lower explosive limits (LEL), oxygen depletion (O2), carbon monoxide (CO), hydrogen sulfide (H2S), and acid vapors is logged throughout the restoration deployment. Complete documentation of all containment boundaries, waste stream manifests, and environmental monitoring logs is compiled daily to satisfy internal EHS audits and regulatory reporting requirements.
Furthermore, all electrical distribution cords, junction splitters, and mobile equipment introduced into the sub-fab utilize Class I, Division 2 explosion-proof rated connections and ground-fault circuit interrupters (GFCI) to prevent accidental static discharge or sparks in sensitive manufacturing sectors.
Emergency exhaust scrubbers and solvent vapor extraction fans must remain operational during water mitigation to ensure worker protection. Our team works hand-in-hand with plant operations to ensure auxiliary drying air currents never counteract chemical exhaust velocity, preserving safe laminar airflow patterns across all hazardous material storage cabinets. Before demobilization, our safety officers conduct formal joint site walks with plant EHS representatives to verify all interlocks, sensor loops, and emergency shutoff mechanisms have been fully re-inspected and re-certified for active production.
Hyper-Local Case Study: Price Corridor Semiconductor Sub-Fab PCW Manifold Failure
Facility Profile & Incident Dispatch Summary
In mid-July, during a prolonged desert heatwave where ambient Chandler temperatures hit 116°F, an advanced 300mm wafer fabrication facility located near Price Road and Dobson Road experienced an abrupt mechanical failure. A 6-inch flanged valve assembly on a primary Process Cooling Water (PCW) supply manifold fractured under pressure surge inside Sub-Fab Basement Sector 3B. Pressurized chilled water (52°F) discharged at approximately 850 gallons per minute into the subterranean utility bay beneath an operating Class 10 photolithography cleanroom suite.
Within twelve minutes of the automated alarm, the facility automated control system throttled the primary supply valve, but an estimated 9,500 gallons of non-deionized industrial process water had accumulated across 14,000 square feet of sub-fab concrete floor area. Water pooled up to 3.5 inches deep in cable trenches, submerging the bases of eight high-voltage dry vacuum pumps and two chemical dispensing skid pedestals. The facility emergency response team immediately mobilized Valley Restoration Pros via our dedicated 24/7 industrial dispatch hotline.
Our industrial response team arrived on site in 28 minutes from our regional deployment depot, integrating seamlessly with client EHS engineers and facility management. Comparable to our large-scale emergency response across Phoenix water damage commercial disasters, immediate containment and extraction operations commenced within forty minutes of initial dispatch.
Psychrometric Metrics & Drying Timeline: Baseline vs. Dry Standard
| Timeline Milestone | Ambient Temp (°F) | Relative Humidity (%) | Humidity Ratio (GPP) | Concrete Slab Moisture (%) | Operational Status |
|---|---|---|---|---|---|
| Hour 0: Initial Inundation | 74°F | 94% | 118 GPP | 100% Saturation (Free Water) | Sector Offline / LOTO Active |
| Hour 4: Bulk Extraction Done | 72°F | 76% | 88 GPP | Surface Dry / Core Wet | Desiccant Array Online |
| Hour 24: Deep Psychrometric Phase | 70°F | 28% | 31 GPP | 78% Internal Slab RH | Vacuum Pump Testing |
| Hour 48: Verified Dry Standard | 68°F | 18% | 18 GPP | 68% Internal Slab RH | Full Fab Production Restored |
By deploying trailer-mounted 10,000 CFM desiccant units and pneumatic extraction pumps within the first hour, Valley Restoration Pros prevented water vapor from entering the overhead waffle slab. Zero photolithography steppers experienced optical fogging or alignment shifts, saving the client an estimated $14.2 million in potential wafer scrapping and tool recalibration expenses.
Follow-up structural laser level surveys confirmed that zero foundation deflection occurred across the massive 36-inch concrete plinths. The sub-fab was returned to full operational readiness twelve hours ahead of the client internal contingency timetable, earning commendations from corporate risk engineering directors.
Post-remediation atmospheric testing conducted forty-eight hours after project completion verified that airborne particulates in the cleanroom remained well within ISO Class 4 requirements, confirming that containment barriers completely isolated the workspace.
Continuous vibration frequency spectrum analysis across all eight dry pump mounting pedestals indicated zero harmonic shift or foundation resonance disruption. The plant insurance carrier accepted our comprehensive documentation binder without deduction, settling the business interruption and emergency property mitigation claim swiftly and transparently.
Commercial Semiconductor Business Interruption & Insurance Itemized Documentation
In the semiconductor fabrication sector, business interruption (BI) claims represent the single largest financial exposure in property loss incidents. With modern 300mm wafer fabs costing upwards of $10 billion to construct and generating tens of millions of dollars in weekly gross revenue, every single hour of line stoppage carries staggering economic implications. Commercial insurers, risk engineers, and forensic accountants scrutinize every facet of an emergency mitigation claim.
Valley Restoration Pros operates with complete billing transparency and regulatory precision. In strict compliance with industry standards, our operations adhere to mandatory disclosure requirements:
- Free Comprehensive On-Site Damage Assessment: Thorough visual, infrared, and psychrometric analysis of all impacted areas without initial inspection charges.
- Transparent Upfront Itemized Pricing Before Work Begins: Every equipment deployment, labor hour, and specialized consumable is clearly enumerated in writing before authorization.
- Assistance with Detailed Claims Documentation & Psychrometric Moisture Logs: Providing verifiable forensic records to facilitate accelerated insurer claim processing without ambiguous billing promises.
We never make misleading representations that insurance will cover 100 percent of costs without client review, nor do we promise direct billing without clear commercial contractual authorization. Instead, we arm facility risk managers with ironclad forensic evidence. Every reading captured by our technicians—from baseline thermal imagery and laser particle counts to in-situ concrete moisture logging (ASTM F2170) and hourly psychrometric drying curves—is compiled into an exhaustive Industrial Disaster Recovery Binder.
This exhaustive documentation bridges the gap between technical disaster recovery and financial indemnification. Forensic accountants and corporate adjusters receive itemized daily work records, equipment run logs with fuel consumption data, calibration certificates for moisture meters and particle counters, and detailed chain-of-custody tracking for all extracted fluid waste streams.
Detailed photographic evidence is indexed by time stamp and specific cleanroom grid coordinates, providing unequivocal visual records of conditions before, during, and after structural decontamination.
Our transparent billing framework avoids blanket lump sums, utilizing standard industry line items that correlate directly to verified psychrometric requirements. This eliminates disputes during insurance audit review and accelerates reimbursement timelines for facility capital expenditure controllers.
To facilitate corporate risk allocation, we provide insurance adjusters with comprehensive root-cause psychrometric mapping, demonstrating exactly how moisture migrated and confirming that structural drying parameters were met without over-drying or material embrittlement. Every piece of equipment deployed is tracked by digital hour meters, and consumable items such as lay-flat ducting and HEPA filters are accounted for with vendor invoices.
Estimates and job summaries are prepared using industry-standard pricing formats (including Xactimate commercial codes and custom industrial time-and-materials schedules). Facility directors seeking a transparent financial projection for facility restoration can utilize our online cost estimator tool to calculate equipment requirements and budgetary parameters.
Exhaustive Semiconductor Sub-Fab Technical FAQ
1. How do you prevent sub-fab moisture from migrating through the waffle slab into Class 1 cleanroom areas?
We establish immediate physical and aerodynamic containment. Technicians seal all waffle slab penetrations, utility pass-throughs, and return air chases with anti-static, fire-rated polyethylene barriers. Industrial HEPA air filtration machines are configured to pull continuous negative air pressure (-0.02 to -0.04 in. w.g.) inside the sub-fab relative to the cleanroom. This pressure differential guarantees that all air currents flow downward from clean zones into the sub-fab, preventing any humid air, aerosolized droplets, or dust from traveling upward into production bays.
2. Can ultra-pure water (UPW) cause electrical or corrosive damage even though it has zero mineral conductivity?
Yes, significantly. While virgin UPW (18.2 Megaohm-cm resistivity) is electrically non-conductive, it is an aggressive, chemically hungry solvent. As soon as UPW spills onto concrete sub-fab floors, structural steel plinths, or dust-covered equipment surfaces, it instantly dissolves minerals, carbon dioxide from the air, and surface residues. Within minutes, its resistivity plummets, transforming it into an electrolytic conductive liquid that short-circuits energized electronics and aggressively attacks metallic contact pins.
3. Why are industrial desiccant dehumidifiers required instead of standard commercial refrigerant units?
Commercial refrigerant dehumidifiers (LGRs) rely on condensation over refrigerated coils and lose efficiency when relative humidity drops below 40% or when ambient temperatures fall below 68°F. Semiconductor sub-fabs require deep drying where dew points must be driven below 30°F and specific humidity drops below 25 GPP to pull trapped moisture out of thick concrete slabs. Desiccant units utilize silica gel adsorption rotors that operate independently of temperature, continuously delivering supply air below 10% RH and sub-freezing dew points.
4. What protocols are followed if cooling tower or chiller lines overflow into the sub-fab?
Cooling tower water contains heavy biocide concentrations, anti-scaling chemicals, and potential biological pathogens such as Legionella pneumophila. When outdoor cooling systems back up into sub-fab utility spaces, we immediately implement protocols matching our commercial cooling tower basin overflow cleanup phoenix procedures. Standing water is classified as Category 3 blackwater, requiring full technician PPE, enclosed chemical extraction, and broad-spectrum antimicrobial decontamination before structural drying commences.
5. How is vibrational stability verified on photolithography plinths after extensive sub-fab drying?
Deep sub-surface moisture saturation can temporarily alter the density and dynamic response of underlying soil and concrete pedestals. Following dry-out, we coordinate with the facility precision metrology engineers to execute dynamic laser interferometry and accelerometer vibration logging across tool support plinths. This verifies that structural resonance characteristics match baseline tool manufacturer specifications (e.g., VC-D or VC-E vibration criteria) before tools are powered up.
6. How do you handle standing water in sub-fab areas adjacent to Toxic Gas Monitoring System (TGMS) sensors?
Water mist or splashing near electrochemical gas sensor heads can foul detector membranes or trigger false gas alarms, initiating unwanted facility emergency shutdowns. Technicians utilize low-pressure, enclosed squeegee vacuum attachments with HEPA-filtered pneumatic vacuum exhausts. Sensor housings in the work zone are protected with breathable hydrophobic shields during extraction, and continuous communication is maintained with the central control room gas monitoring operator.
Chandler Semiconductor Corridor Logistics & Valley-Wide High-Tech Coverage
The Chandler Silicon Corridor encompasses a dense cluster of microelectronics design, manufacturing, and advanced packaging infrastructure. Centered along the Price Road technology spine between the Loop 101, Loop 202 Santan Freeway, and Queen Creek Road, this high-density industrial corridor demands instant logistics deployment. When an industrial water catastrophe occurs, every minute lost in transit amplifies cleanroom risk and compounding financial losses.
Valley Restoration Pros maintains strategically pre-staged commercial rapid-response equipment hubs positioned directly adjacent to major East Valley transportation corridors. From our East Valley staging depot near Chandler Boulevard and the Loop 101, our commercial desiccant trailers, heavy vacuum plants, and IICRC-certified technical squads achieve guaranteed 30-minute rapid response times to any high-tech facility along Price Road, Dobson Road, and the Ocotillo production corridor.
Our industrial disaster response capabilities extend across all major technology and industrial manufacturing corridors throughout the Greater Phoenix metropolitan area. From the advanced semiconductor supply chain facilities in nearby Tempe water damage response zones to the defense aviation and aerospace hubs in Mesa water damage territories and the massive north Phoenix semiconductor development cluster along the Loop 303 corridor, our mobile industrial fleet delivers unparalleled technical restoration depth.
Each mobile response trailer carries self-contained electrical generation assets, auxiliary fuel supplies, cleanroom pass-through ducting, and a complete inventory of ESD-compliant containment barriers. We maintain continuous operational coordination with local municipal emergency management and utility providers across the Valley, ensuring unobstructed site access and rapid operational clearance during critical industrial loss incidents.
Whether mitigating a high-pressure line failure, neutral basin overflow, or monsoon deluge intrusion, our team provides 24-hour command structure oversight, ensuring uninterrupted communication between cleanroom facility directors, risk adjusters, and on-site restoration crews.
We actively maintain pre-emergency service level agreements (SLAs) with technology corridor operators, ensuring priority mobilization and equipment reservation during regional weather crises or municipal water anomalies.
Immediate Commercial Semiconductor Sub-Fab Dispatch: 24/7/365
When process cooling water breaches, cleanroom plenum humidity rises, or subterranean utility vaults flood along the Chandler Price Corridor, our Master Certified industrial response units are standing by for immediate mobilization.
Verified Local Area Dispatch: Chandler, AZ
Official Geo-Coordinates: 33.3062° N, -111.8413° W • Maricopa County
Related Specialized Emergency Restoration Services
Explore specialized rapid-response mitigation protocols across Greater Phoenix and Maricopa County:
Valley-Wide Emergency Response Service Coverage
Our mobile restoration fleet is dispatched across the entire Phoenix metropolitan region, providing rapid 30 to 60 minute emergency response: